

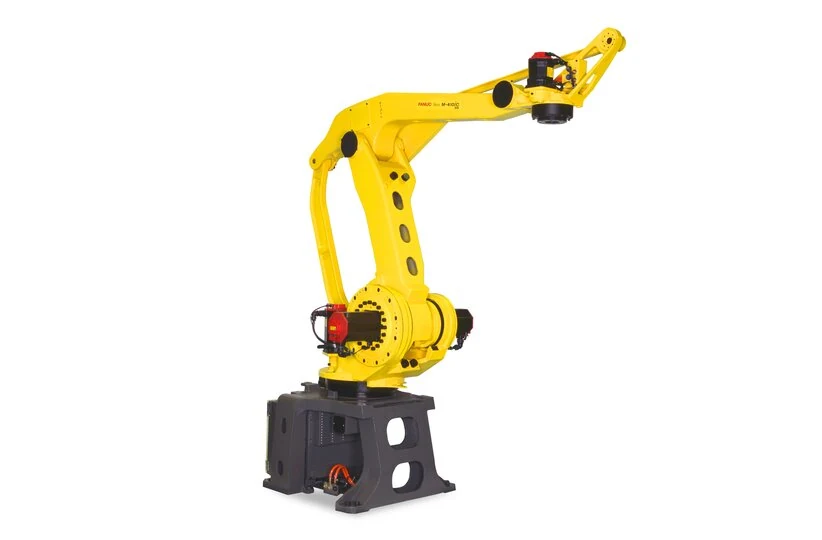
FANUC M-410iC/315 palletizing errors should be described by their pattern. A whole pallet shifted in one direction, alternate layers rotated incorrectly and cartons drifting after release are different faults. Retouching every placement point can hide the pattern that would otherwise locate the cause. Keep the original recipe and record the first incorrect placement.
Confirm the complete M-410iC/315 model, controller and application setup. A related M-410 family name does not establish identical geometry or load conditions. The end effector, pallet conveyor and pattern software may be supplied separately. Use the installed documents for their coordinate definitions, interfaces and permitted operations.
Classify the first incorrect layer
Record the pallet identifier, pattern, layer number, item index and tool orientation. Measure against a defined pallet feature rather than an unstable carton edge. Note whether the same logical position is wrong on every pallet. A recipe indexing error can affect a repeatable layer even when the robot repeats each requested coordinate accurately.
- Save the selected recipe, current item count and active pallet reference.
- Keep pickup and placement observations separate.
- Record pallet locating and conveyor stop conditions.
- Note carton size, weight, surface and recent tooling changes.
Check physical pallet locating before software offsets
After the equipment is secured, inspect stops, locating devices and the supported pallet surface. A pallet that settles differently can shift every layer relative to the cell. Compare the original locating feature with the actual carrier and pallet type. A valid pallet-present sensor may indicate only that a pallet exists, not that it is accurately seated.
Check whether the program selected the intended pallet reference and active station. A correct coordinate for station A can be wrong at station B. Preserve the previous reference and selection logic before any approved correction. Do not compensate a loose stop by adding an unexplained position shift to the recipe.
Review layer, item and orientation data
Compare the intended pattern with the active recipe, including carton dimensions, gaps, layer height and rotations. Track the item index through completion and the next-cycle increment. If a stopped cycle is resumed, verify how the application retains that index. A duplicated or skipped item may originate in recovery logic rather than positioning hardware.
| Pattern | Useful comparison | Next work boundary |
|---|---|---|
| All layers shifted together | Pallet locating and active reference | Fixture or reference correction |
| Only alternate layers rotated | Recipe orientation and layer index | Pattern logic |
| Height error grows with layers | Actual carton height and recipe increment | Dimensional setup or compression review |
| Part shifts after release | Tool release, carton surface and support | Gripper and placement method |
Separate robot position from carton movement
Compare where the tool is when placement ends with where the carton is after release. A worn gripping surface, incomplete release or side contact can move the carton without a robot position error. Review pneumatic or vacuum feedback if fitted. An end-effector closed or open signal does not prove that the carried item stayed at the intended location.
Inspect the tool mounting, fingers, suction elements and service routing under the approved isolation procedure. Keep the actual load, center of gravity and inertia within the documented application envelope. Reducing speed may change the symptom but does not identify the cause. The correction should address the supported finding rather than an assumed mechanical weakness.
Decide whether a robot component needs repair
If the fixture, recipe and holding conditions agree but the measured tool position is inconsistent, review the relevant robot motion with the installed diagnostic and maintenance procedures. A component decision needs supporting mechanical or feedback evidence. A layer offset alone is not proof of a worn gearbox, failed encoder or lost robot calibration.
Keep software corrections and physical repairs separately identified. Record the original and revised recipe, fixed locating parts and any robot component work. Preserve the application backup before changes. If referencing or calibration is required after an identified repair, use the applicable procedure and document the reason it was needed.
Verify a complete representative pallet
A single corrected placement cannot verify the pattern. Use the agreed carton and pallet arrangement to check pickup, each relevant layer transition, placement and release. Include the application recovery condition that produced the complaint. Inspect the actual completed arrangement with the agreed dimensional and stability criteria, without putting people under suspended or unsecured loads.
Record recipe and reference versions, item counts, measurement results and the pass criteria. A component bench test does not validate carton deformation, pallet locating or the complete production cycle. For a service assessment, send these records with full model labels and the first affected layer. That defines whether the work belongs to robot repair, tooling or line integration.
Check layer indexing and accumulated height explicitly
For a simplified uniform stack, a layer reference may be expressed as z equals z0 plus n multiplied by h. Define z and h in the same length unit, z0 as the first layer reference and n as an index starting at zero. This is an illustrative model, not the installed FANUC program. Confirm whether the actual application uses a different index convention or pattern-specific heights.
A constant initial error and a growing height error point toward different comparisons. Measure the actual cartons and supporting surface, including relevant compression, before correcting h. A plausible calculation cannot establish that a damaged locating device or slipping gripper is healthy.
Palletizing robot inspection and repair
FANUC M-410iC/315 maintenance checks
Contact Suntech with the layer and recipe record